
E-mail:
david@wuyunconveyor.com

REQUEST A QUOTE
ENG
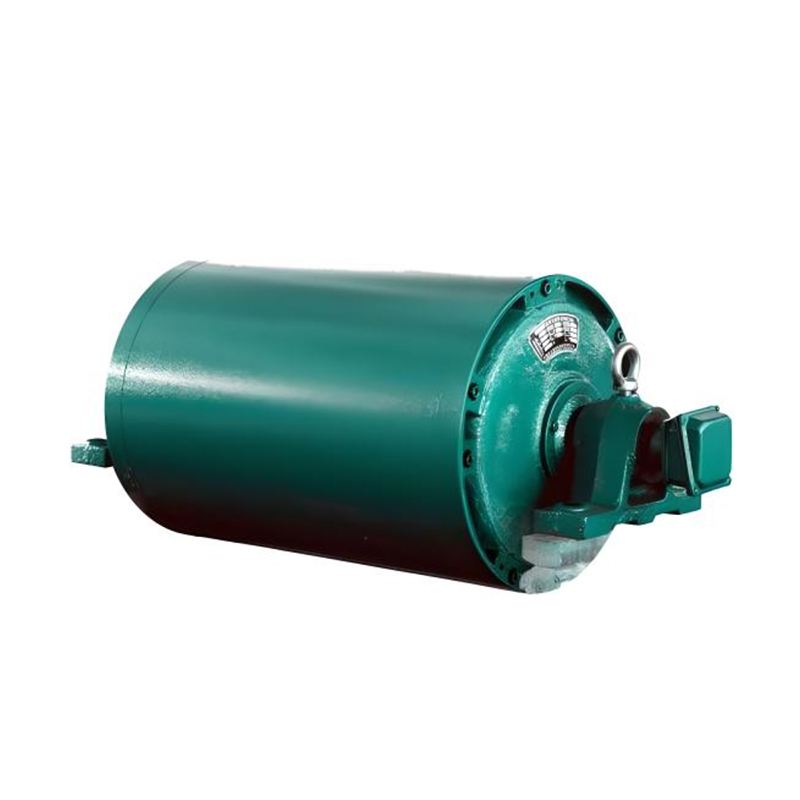
The Conveyor Motorized Pulley is an integrated drive unit for belt conveyor systems, with the electric motor and gearbox enclosed within the pulley shell. This all-in-one design combines the conveyor drive and pulley into a compact unit, eliminating the need for separate external motor and gearbox assemblies.
By integrating the drive components inside the pulley, the Conveyor Motorized Pulley provides a compact conveyor drive solution while reducing exposed transmission components. Its enclosed structure is also well suited to demanding industrial environments where protection against external contaminants is required.
Key Features
Integrated Drive Design
The electric motor and gearbox are integrated inside the pulley shell, creating a compact all-in-one conveyor drive unit.
Space-Saving Structure
The integrated design eliminates the need for separate external drive components, helping reduce the installation footprint of the conveyor drive system.
Enclosed Drive Components
The internal motor and gearbox are protected within the pulley shell, reducing exposure to dust, moisture, abrasive materials, and other external contaminants.
Direct Conveyor Drive
The motorized pulley functions as the conveyor drive itself, transmitting driving torque directly through the pulley to the conveyor belt.
Compact Conveyor Integration
The integrated construction simplifies the overall conveyor drive arrangement and is particularly useful where installation space is limited.
Product Advantages
Compact drive solution: Integrates the motor, gearbox, and pulley into one unit.
Space saving: Reduces the footprint required for conventional external drive arrangements.
Reduced exposed components: Encloses major drive components within the pulley shell.
Simplified conveyor design: Reduces the number of external transmission components required.
Reliable operation: The enclosed structure helps protect internal components from demanding environmental conditions.
Low maintenance potential: The integrated design reduces exposed transmission components and simplifies the overall drive arrangement.
Applications
The Conveyor Motorized Pulley is designed for belt conveyor systems where a compact, integrated drive arrangement is preferred. Its enclosed motor and gearbox make it suitable for applications where installation space is limited or where exposed drive components could be affected by dust, moisture, abrasive materials, or other harsh operating conditions.
Typical applications include:
Mining and Quarrying: Suitable for bulk material conveyors handling ores, aggregates, crushed stone, and other abrasive materials.
Cement and Building Materials: Used in continuous conveying systems where compact drive integration and environmental protection are important.
Coal Handling: Suitable for bulk material conveyors operating in dusty industrial environments.
Ports and Bulk Material Handling: Used in conveyor systems where compact drive arrangements and reliable continuous operation are required.
Steel and Metallurgy: Suitable for demanding industrial conveying applications requiring an enclosed conveyor drive.
General Industrial Conveying: Applicable to belt conveyors where installation space, simplified drive arrangement, and protection of drive components are important.
Ordering & Quotation Information
Information Required for Quotation
Please provide the required pulley size, conveyor belt width, operating requirements, installation position, required quantity, and operating environment. Power supply requirements and existing drawings or photos should be provided where applicable.
Technical Confirmation & Lead Time
We will confirm the motorized pulley configuration according to conveyor arrangement, belt width, operating requirements, installation interface, and environmental conditions. Lead time depends on configuration, quantity, material preparation, and purchased components.
Packaging, Delivery & Quality
Packaging and delivery are arranged according to product dimensions, weight, quantity, transportation method, and destination. Product configuration, quantity, appearance, and packaging completeness are checked before shipment.
FAQ
What is a Conveyor Motorized Pulley?
A Conveyor Motorized Pulley is an integrated belt conveyor drive unit that houses the electric motor and gearbox inside the pulley shell.
What is another name for a motorized pulley?
A motorized pulley is also commonly referred to as a Drum Motor or Motorized Drum in the conveyor industry.
What is the advantage of integrating the motor and gearbox inside the pulley?
The integrated design creates a compact drive unit, reduces the need for external transmission components, and saves installation space.
Is a motorized pulley suitable for harsh environments?
The enclosed drive structure helps protect internal components from dust, moisture, abrasive materials, and other external influences, making motorized pulleys suitable for demanding industrial conveyor applications.
Does a motorized pulley replace a conventional external drive?
Yes. A motorized pulley integrates the drive motor and gearbox into the pulley itself, eliminating the need for a separate external motor and gearbox arrangement.
Where are motorized pulleys commonly used?
They are widely used in mining, quarrying, cement, ports, coal handling, and other bulk material conveying applications.
technological innovation, keep improving
With ingenuity, we are committed to global sustainable development.
Professional Conveyor Manufacturer, Since 1998.
Mobile QR Code
News & Updates
Contact infor.
 Phone / Whatsapp:
 Tel: +86-0519-86511555
 E-mail: david@wuyunconveyor.com
 Add: No.16 Xinfa Road, Wujin District, Changzhou City, Jiangsu Province, China
 English